Plastic Profile Machine Maker Guide to Boost Your Production Efficiency
2026-09-05
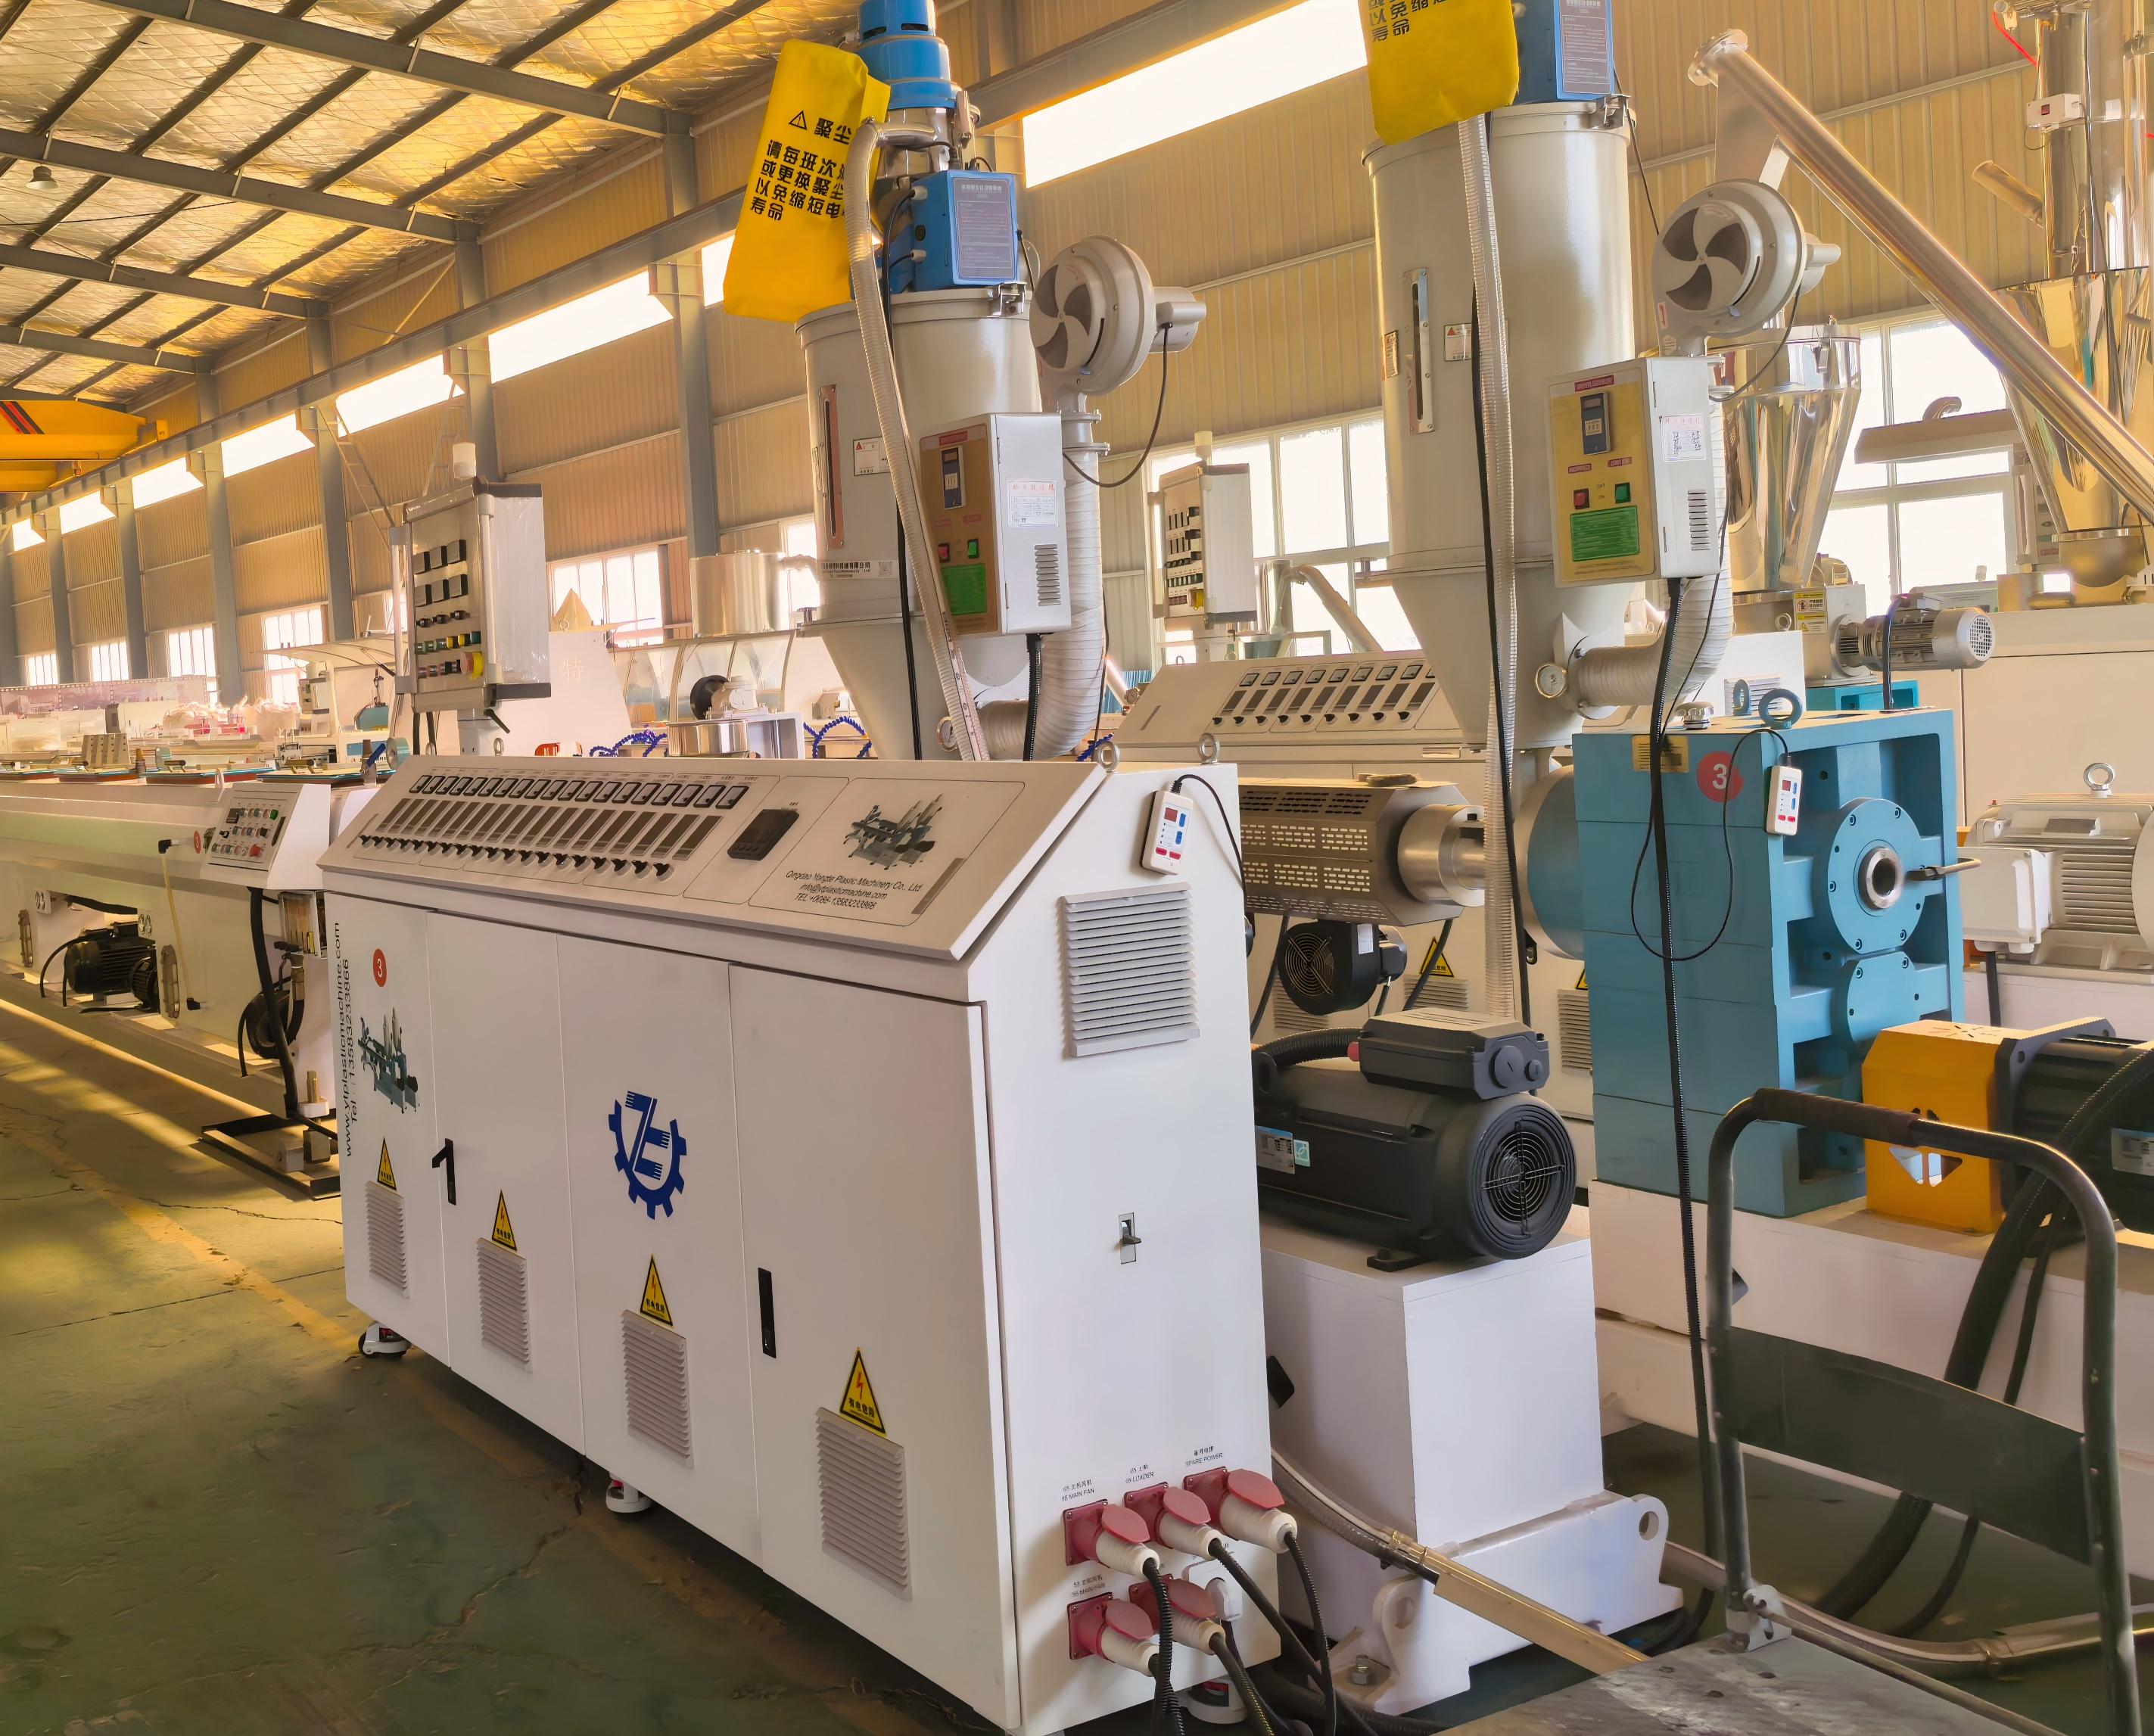
Every stalled extrusion line and every rejected profile cuts directly into your margins. Yet most production guides recycle the same generic advice. This one doesn’t. Built from field data and real machine behavior, it breaks down where plastic profile manufacturing actually loses time—from screw design and die tuning to cooling calibration and haul-off sync. You’ll find concrete adjustments you can test this week, not theory. And because the right equipment partner matters as much as the right settings, we’ve included insights shaped by Yongte’s engineering team, who’ve spent years solving these exact bottlenecks for profile producers. If you’re ready to move beyond incremental tweaks and see measurable output gains, keep reading.
Start With the Melt, Not the Machine
Most troubleshooting sessions begin the wrong way around. Someone sees a short shot or a warped part and immediately reaches for the injection speed dial or starts tweaking barrel temperatures zone by zone. That approach assumes the machine is the source of truth. It is not. The machine only does what the melt allows it to do. Before touching a single setting, ask what the polymer itself is experiencing: is the melt uniformly heated, or does it carry cold slugs and thermal streaks? Has the material been dried properly, or is moisture turning to steam inside the screw? A melt that arrives at the nozzle with inconsistent viscosity will never produce consistent parts, no matter how carefully the clamp force or hold pressure is dialed in.
Think of the melt as the message and the machine as the messenger. If the message is garbled—too stiff in one region, too runny in another, or partially degraded from excessive residence time—the messenger cannot fix it. Adjusting back pressure or screw speed might mask a problem for a few cycles, but the root cause remains in the material's thermal and shear history. The most valuable skill in a processing environment is learning to read the melt: watching how it flows from a purge, checking for unmelted pellets or bubbles, and noticing whether the sprue breaks clean or strings out. Those observations tell you far more than a dozen machine parameter changes. Once the melt is right, the machine settings almost fall into place on their own.
Match the Screw to the Resin You Actually Run
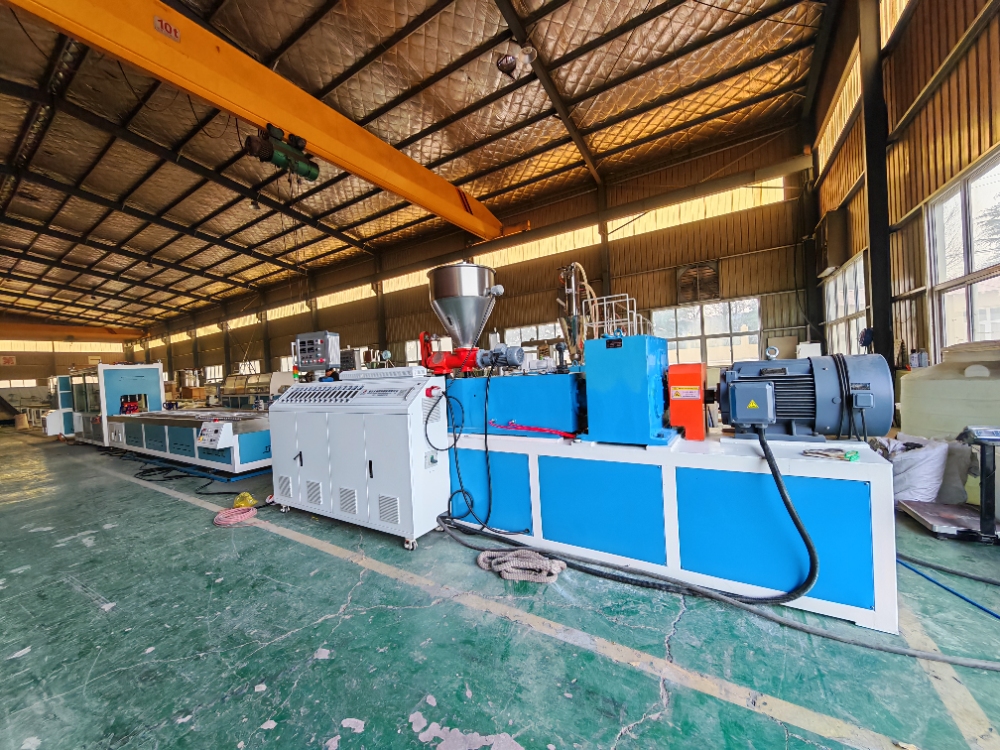
Most shops grab a general purpose screw and wonder why the melt temperature swings or the color change takes forever. The screw is not a universal part. If you run nylon with glass fiber, a standard metering section will chew up the fiber length and leave you with weak parts. A low-compression screw with a deeper flight in the feed zone preserves glass and keeps the viscosity from spiking. Polycarbonate, on the other hand, hates shear heat. A screw with a longer compression section and a gentle transition keeps the material from yellowing at the barrel wall.
Polypropylene and polyethylene are forgiving, but they still benefit from a barrier screw when you push high throughput. The barrier flight separates the melt pool from the solid bed, so you avoid the classic “unmelted pellet in the middle” defect. For sticky engineering resins like PBT or PET, a screw with a mixing torpedo or a Maddock section breaks up the thermal gradient without overworking the polymer. The trick is to match the screw’s compression ratio to the resin’s melt density—not the solid density printed on the bag.
Before you order a new screw, pull the last three jobs you actually ran. Write down the resin family, the melt index, and whether it had fillers or flame retardants. Then compare that list to your current screw’s L/D, compression ratio, and mixing section. If your screw was designed for ABS but you now run mostly glass-filled nylon, the wear on the root diameter will be uneven and the recovery time will creep up. Swap the screw to match the resin, and the same machine will hold a tighter cushion and drop the scrap rate without touching the barrel temperatures.
Cooling Tweaks That Add Meters Per Minute
Most riders chase speed by pushing harder on the pedals, but heat buildup quietly destroys that effort. As core temperature rises, blood diverts to the skin for cooling, leaving less oxygen for working muscles. The result is a drop in sustainable power that no amount of motivation can override. A few practical cooling adjustments, however, can keep that thermal ceiling higher and translate directly into extra meters per minute on the road or trail.
Start with the obvious but often ignored: dumping heat before it accumulates. A pre-ride ice vest or a cool shower lowers starting core temperature, buying you a larger buffer before performance fades. During the ride, prioritize airflow over aerodynamics when speeds are low or climbs are long. Unzip jersey fronts just enough to let air swirl across the chest and neck, where large veins sit close to the surface. Switch to lighter, open-weave fabrics and consider wetting your forearms or the back of your neck at feed zones—evaporation does the heavy lifting without adding drag.
Don't overlook internal cooling. Hydration with chilled fluids works from the inside out, and drinking small amounts frequently prevents the gut from pooling warm liquid. Electrolyte balance also matters: sodium helps retain fluid in the bloodstream, keeping sweat rates efficient instead of thick and sluggish. Even simple timing shifts help. Save the hardest efforts for cooler parts of the day or after a brief shaded descent. Each small tweak on its own seems trivial, but combined they can easily add the equivalent of two or three bike lengths every minute.
Feeder Calibration Drift Is Stealing Your Output
You’ve tuned every parameter, swapped out worn nozzles, and double-checked your material specs, yet the parts keep coming out slightly off—walls a touch thicker here, a hint of under-extrusion there. The culprit rarely announces itself. Feeder calibration drift happens when the actual material output per step gradually deviates from the value your firmware expects, often due to thermal expansion, gear wear, or tension shifts in the filament path. It’s not a dramatic failure; it’s a slow bleed that shaves precision off every single layer.
The insidious part is that drift compounds across long prints. A 2% over-extrusion on the first hour might look acceptable, but by hour six it has pushed enough extra plastic into the part to distort dimensions, clog fine details, and stress the frame. Operators tend to blame the slicer, the ambient temperature, or even the filament batch before they suspect the feeder itself. Regular calibration checks with a precise scale or a measured extrusion test can catch the drift early, but many shops still rely on a set-and-forget approach that quietly costs them yield.
What separates top-performing lines isn’t better hardware—it’s the habit of treating feeder calibration as a living value, not a static offset. Log the measured steps per millimeter each week, track the trend, and adjust before the drift becomes visible in the finished product. A few minutes of verification at the start of a shift can save reprints, scrap, and the slow erosion of your throughput that nobody puts on a downtime report.
Why Profile Defects Often Trace Back to Die Wear
In the extrusion bay, operators often chase temperature, ram speed, or billet chemistry before thinking about the die itself. Yet many surface streaks, wavy edges, or local thinning can be traced straight back to the condition of the die bearing. Once the bearing edges start to wear, metal flow loses its uniformity, and the once-crisp profile begins to drift. These small deviations stack up fast, turning into visible defects that no amount of process tweaking can fully hide.
Die wear rarely announces itself with a bang. It creeps in through repeated thermal cycles and high-pressure friction, gradually eroding the nitrided layer that protects the working surface. Once that hard shell is gone, the softer steel underneath wears at an accelerated pace, and the profile starts showing periodic blemishes—glossy patches, faint grooves, or dimensional drift. What makes it tricky is that wear tends to concentrate in a few stubborn spots, like narrow slots or sharp corners, so the same defect keeps popping up in the same place on every run.
Instead of waiting for a pile of scrap to force the issue, a simple tracking habit can save a lot of pain. Logging press tonnage, surface finish changes, and die repairs after each run gives a clear picture of when a die is nearing its wear limit. Swapping in a re-nitrided die or touching up the bearing often clears up contour defects far more reliably than chasing every other variable on the line.
Operator Habits That Keep Lines Running Through Shift Changes
A smooth handoff rarely happens by accident. The best operators treat the last thirty minutes of their shift as a live briefing, not a countdown. They walk the line with the incoming crew, pointing out the small stuff that never makes it into the logbook: a slight vibration on conveyor three, a die that needs watching after lunch, a sensor that trips if the humidity climbs too high. These walk-and-talk habits turn tribal knowledge into shared knowledge, so the next shift isn't starting from zero.
Clear notes matter, but structure matters more. Operators who keep lines running use a simple handoff format: what ran well, what almost failed, what's due next, and what needs eyes in the first hour. They don't bury the important details in paragraphs. Instead, they mark the line-side board with a quick sketch or a flagged tag. That way, a tired incoming tech can scan the situation in ten seconds and still catch the one thing that would have shut them down at 2 a.m.
Finally, the best operators don't just hand off problems; they hand off options. If a line is limping on reduced speed, the outgoing shift leaves a note on what they tried, what they ruled out, and what they'd do next with another pair of hands. That kind of forward-looking habit cuts the restart learning curve and keeps small issues from becoming overnight downtime.
FAQ
Look beyond horsepower and screw diameter. Check whether the barrel has enough heating zones for your material's melt profile and whether the screw L/D ratio suits the compounds you run. A machine with a grooved feed throat can give you higher throughput on certain rigid formulations, but it may not be worth the extra cost if you switch materials often. Ask the maker to provide actual throughput data with a similar profile, not just theoretical numbers.
Focus on the parts that wear unevenly, like screw flights and barrel liners, rather than just greasing fittings. Monitoring melt pressure before and after the screen pack reveals when buildup is forcing the extruder to work harder. A simple weekly check of vacuum calibration tank seals and water flow can prevent a lot of sudden line stops. Keep a log of each heating zone's current draw; a drift usually means a failing heater or poor contact before it becomes a full failure.
The screw is where most output gains hide. A barrier screw with a dedicated melt channel can deliver more uniform temperature and fewer gels, letting you push the line faster without surface defects. If you're running recycled material, a vented screw with a longer compression section helps pull moisture and volatiles before they reach the die. Don't assume a general-purpose screw is fine for every profile—having one spare screw tuned to your highest-volume product can pay for itself within months.
Yes, but the biggest time sink is rarely the die swap itself; it's recalibrating the cooling and haul-off. Use pre-set die carts that keep the die, adapter, and calibration blocks aligned together so you're not reassembling from scratch. Mark a reference position on the calibrator slides for each profile. If your runs are short, consider a dual-head setup or a quick-clamp system for the die, which reduces thermal cycling and keeps the melt more stable.
Downstream equipment does more than pull the profile—it locks the shape. Vacuum calibration with properly placed slots and enough zones can eliminate sag and bowing that lead to high scrap. Check that the first calibration block sits close enough to the die, otherwise the hot profile will sag before it's set. Adding a closed-loop water temperature control to the calibration bath keeps cooling consistent, which matters more than people realize for dimensions and gloss.
Start with automatic gauge control if your profiles need tight tolerances; it adjusts haul-off speed based on laser or contact measurement, reducing manual sampling. A gravimetric feeder that doses material by weight rather than volume prevents surging when bulk density shifts. Even a simple automatic cut-to-length saw with encoder feedback saves labor and cuts scrap from mis-measured parts. Avoid full robotic packing until you've fixed the upstream variability—automation works best on a stable line.
Use the resin supplier's recommended range as a starting point, then measure melt temperature directly with a hand-held probe rather than trusting barrel setpoints. Settings are often too high because operators compensate for poor screw cooling or worn heaters. Reduce the rear zone temperature in small steps while watching melt pressure; lower temps can actually improve melt strength for profiles if the screw can still convey the material. Never drop the die temperature below the melt's freeze point just to speed cooling—that creates internal stress and warpage later.
Heating and cooling can fight each other if the barrel insulation is damaged or missing. Insulate the die and adapter, and reclaim heat from the cooling tanks for building or water preheating. Oversized motors running at low load waste electricity; a variable-frequency drive on the extruder and haul-off lets you match power to actual demand. Check for compressed air leaks near the calibration table—small leaks add up to a surprising amount of energy and can also destabilize the vacuum.
Conclusion
Start with the melt, not the machine. A stable, homogeneous melt can mask many downstream issues, so verify barrel temperature profiles, screw recovery time, and back pressure before touching hardware. Then match the screw design to the resin you actually run—not the grade on the original spec sheet. Additives, recycled content, or even lot-to-lot viscosity shifts require different compression ratios and mixing sections. Cooling tweaks are often the cheapest speed upgrade: stagger water tank temperatures, fine-tune vacuum sizing, and adjust spray patterns to add meters per minute, especially on thin-walled or hollow profiles where heat removal limits line speed.
Feeder calibration drift quietly steals output because throughput is rarely checked after initial setup. Schedule weekly gravimetric verification and calibrate on the actual blend, not a virgin reference. Profile defects frequently trace back to die wear rather than process settings—inspect land lengths, chrome plating, and lip edges regularly; early signs like edge tearing, surface haze, or dimensional drift are cheaper to fix before they become scrap. Operator habits matter just as much: clear start-up checklists, recorded die gap offsets, and a concise five-minute handover note keep lines running through shift changes. These small, consistent adjustments compound into significant efficiency gains without major capital investment.
Contact Us
Contact Person: Ms Qin
Email: [email protected]
Tel/WhatsApp: 8613583233866
Website: https://www.yongteplast.com